Laboratory Centrifuges
Advanced Centrifuge Machines for Laboratory Applications
Labtronixed Inc. manufactures a comprehensive range of high-quality centrifuge machines designed to meet the diverse requirements of laboratories, research centers, hospitals, diagnostic facilities, pharmaceutical industries, biotechnology laboratories, and scientific institutions. Our centrifuges are developed with a focus on reliable performance, precise speed control, smooth operation, safety, and long-term durability. The Labtronixed Inc. centrifuge range includes Mini Centrifuges, Micro Centrifuges, Refrigerated Centrifuges, Universal Refrigerated Centrifuges, Micro Plate Refrigerated Centrifuges, Floor Model Refrigerated Centrifuges, and High-Speed Centrifuges, available in different RPM configurations to suit specific laboratory applications.
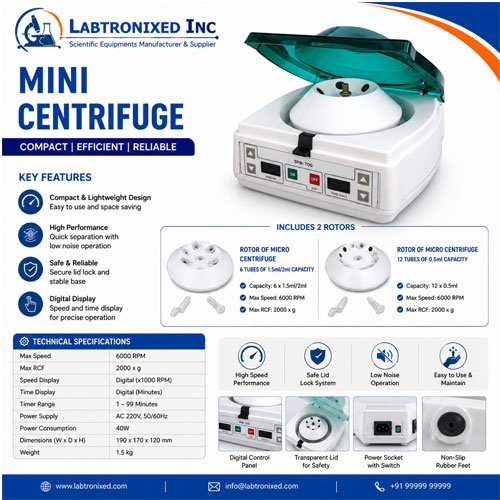
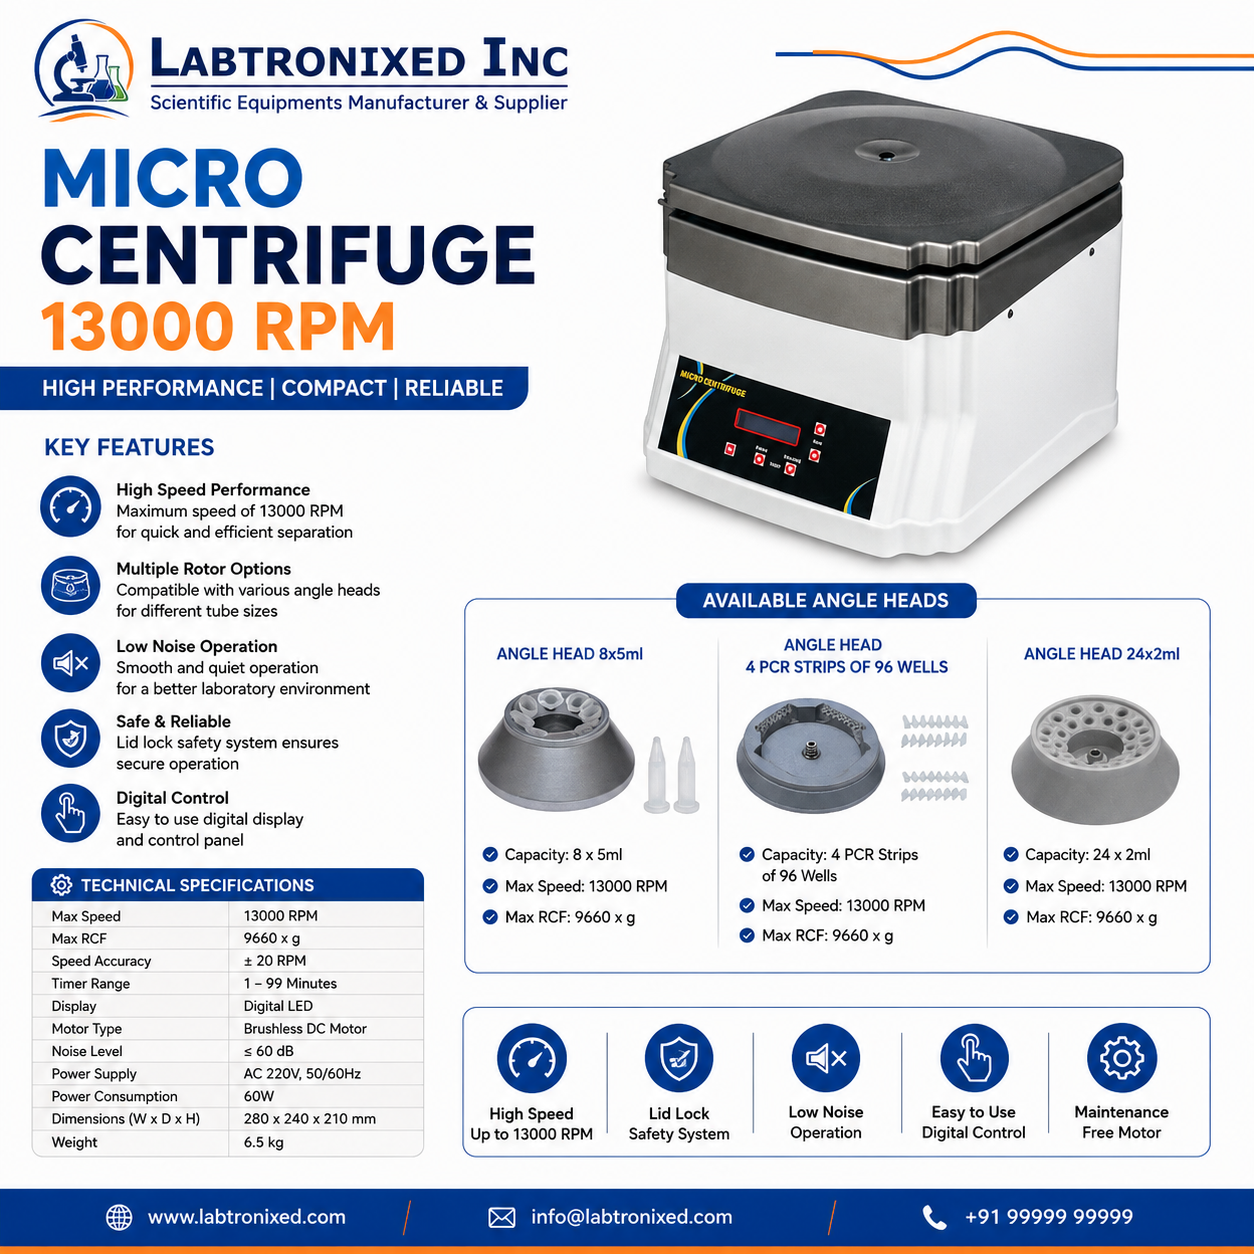
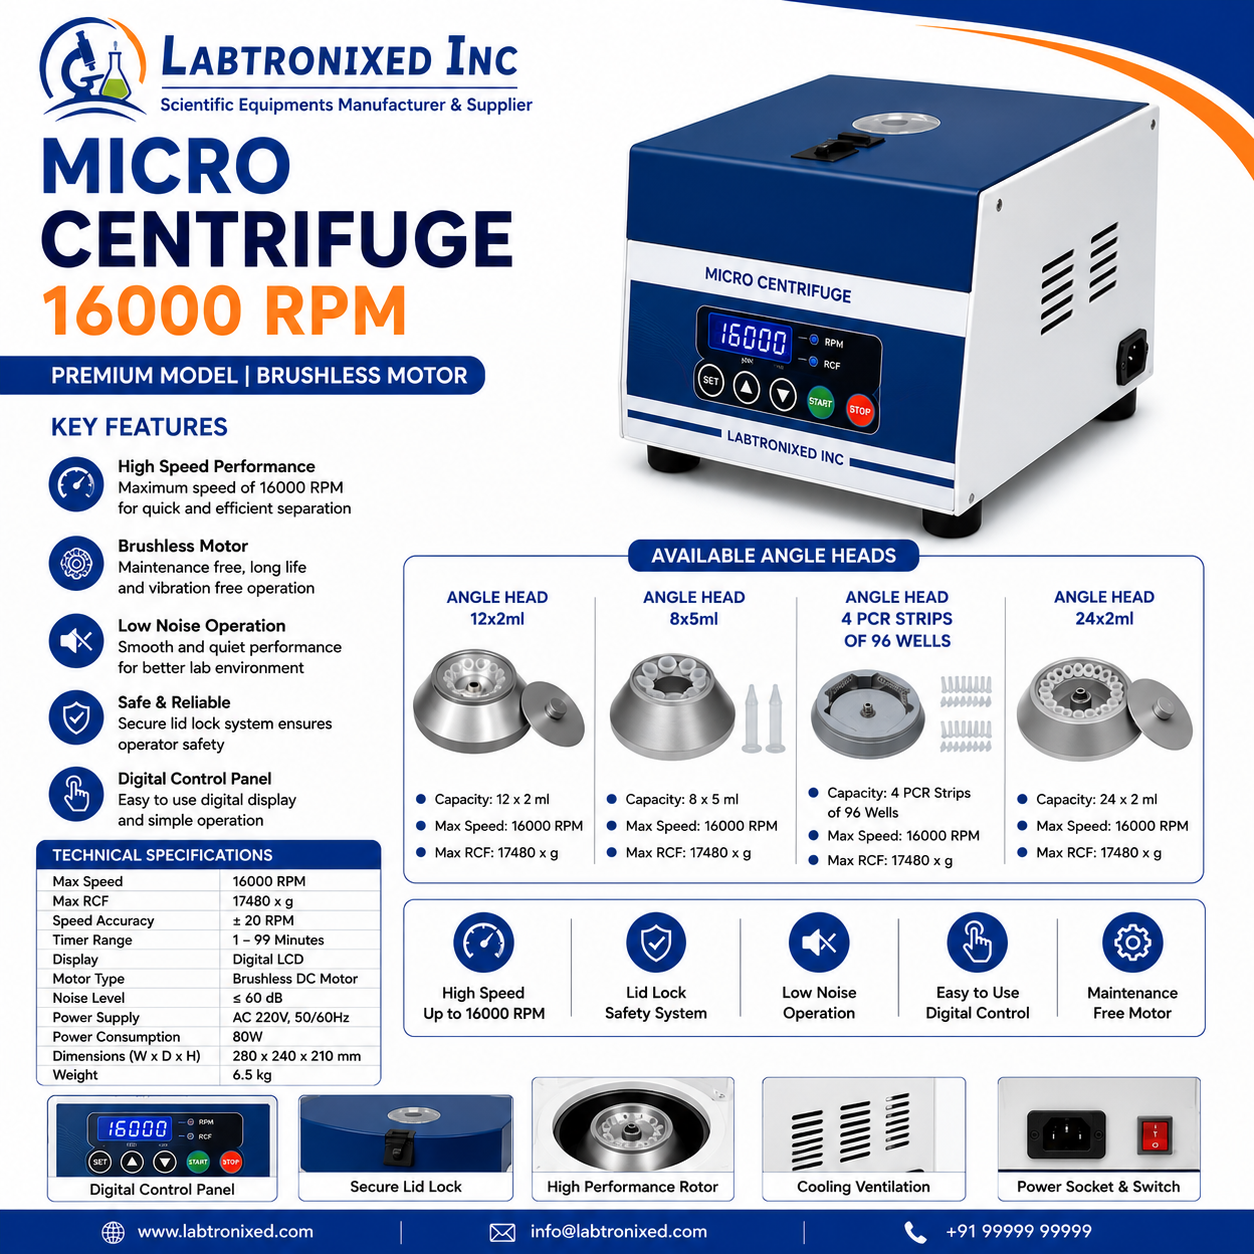
Our Mini Centrifuge is a compact and efficient solution for routine laboratory applications where space-saving design and quick sample processing are important. For applications requiring higher centrifugal force, Labtronixed Inc. offers Micro Centrifuges with speeds of 13,000 RPM, 16,000 RPM, and 20,000 RPM. These models are suitable for molecular biology, biotechnology, research, diagnostic, and other laboratory procedures where rapid and efficient separation of samples is required.
For temperature-sensitive samples, our Micro Refrigerated Centrifuges are available in 16,000 RPM and 20,000 RPM configurations. These centrifuges combine high-speed performance with effective temperature control, helping laboratories maintain sample integrity during centrifugation. Our Universal Refrigerated Centrifuge 1600 RPM and Universal Refrigerated Centrifuge 20,000 RPM provide versatile solutions for laboratories with different sample processing requirements. Selected models feature microprocessor-based control and brushless motor technology for reliable, low-maintenance, and efficient operation.
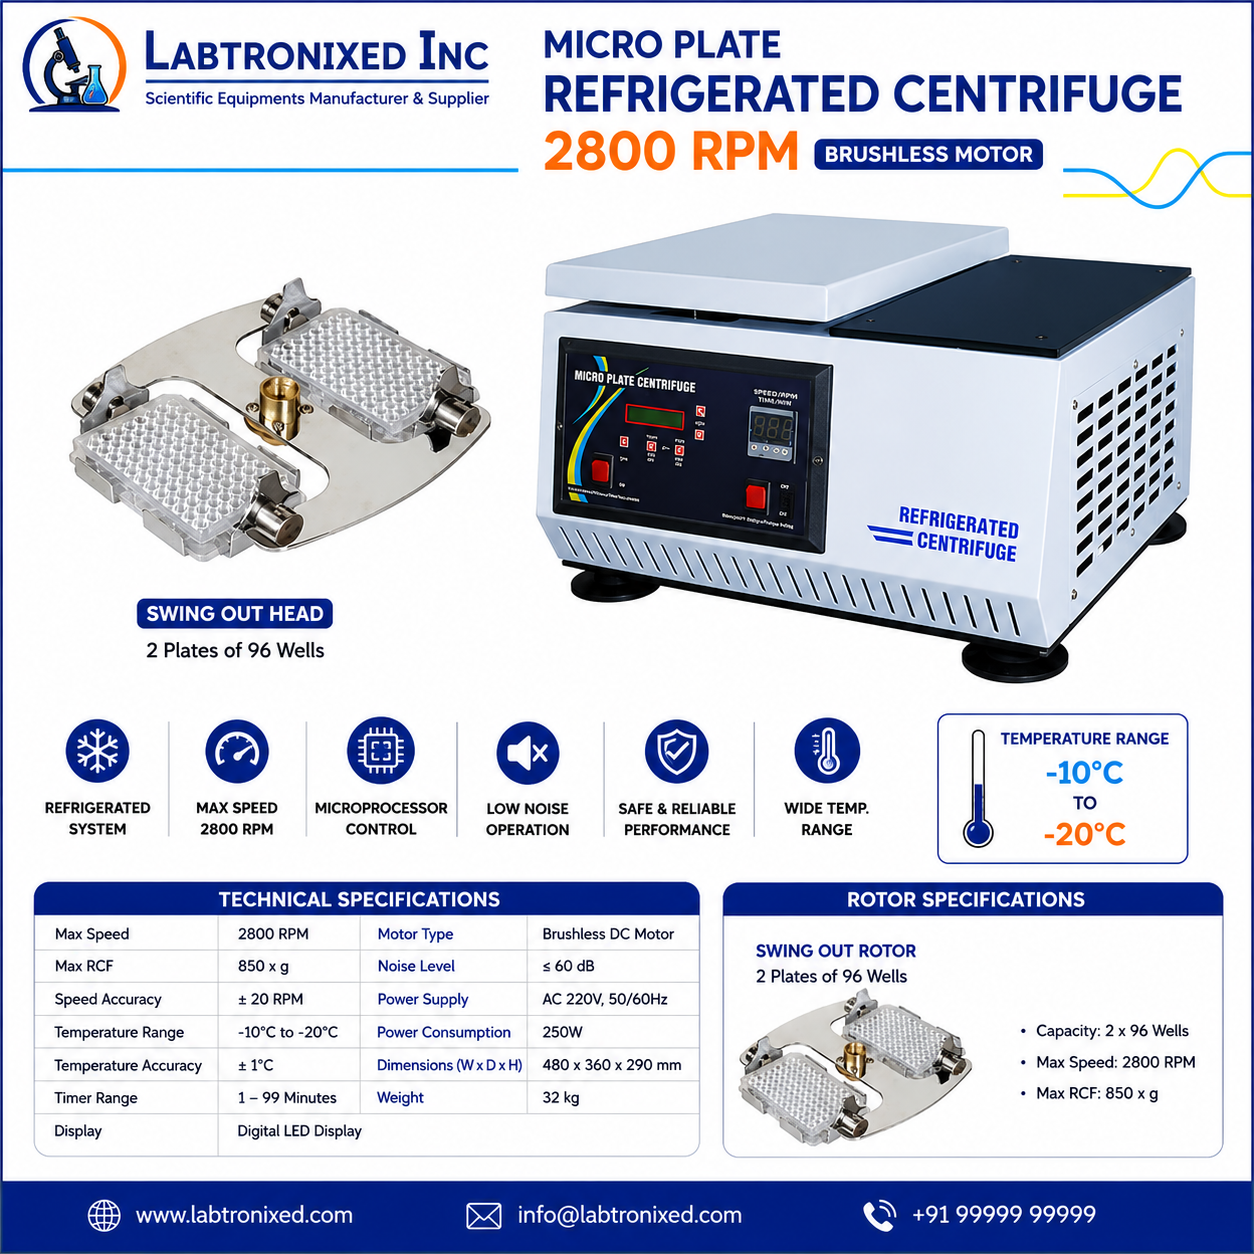
We also manufacture Micro Plate Refrigerated Centrifuges with 2,800 RPM brushless motors, designed for applications involving microplates and temperature-sensitive samples. Their refrigerated operation and controlled centrifugation make them suitable for research, diagnostic, biotechnology, and pharmaceutical laboratory applications.
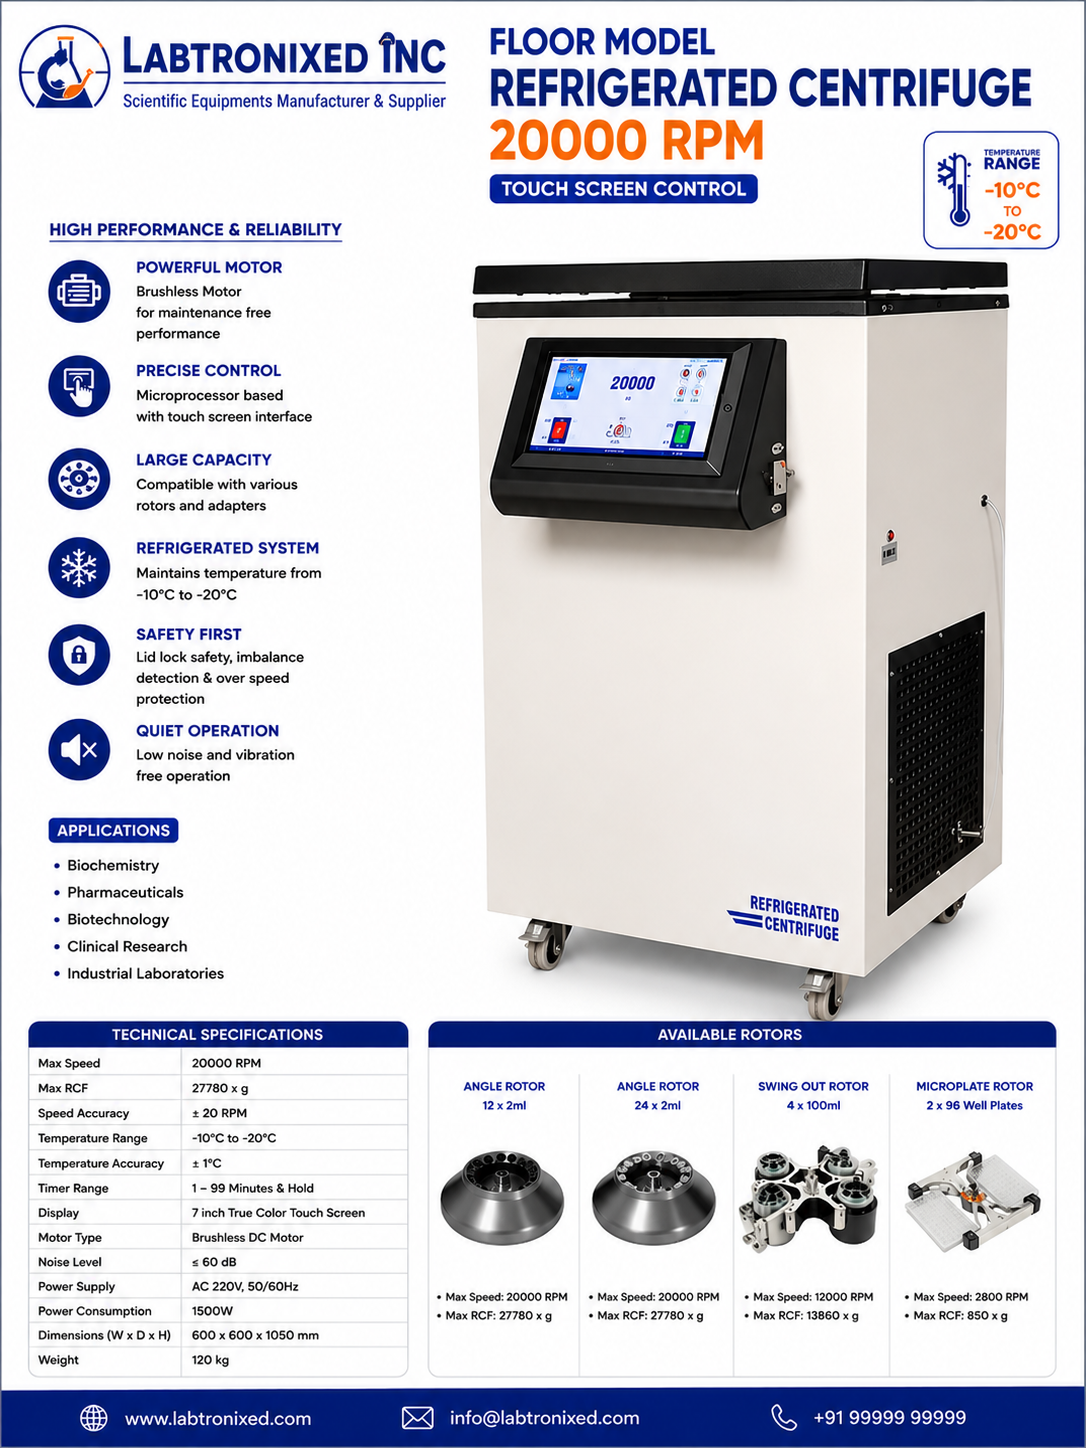
For laboratories requiring higher capacity and advanced operation, the Labtronixed Inc. Floor Model Refrigerated Centrifuge with speeds up to 20,000 RPM and Touch Screen control provides a modern solution for demanding centrifugation requirements. The user-friendly touchscreen interface allows convenient operation and monitoring, while the refrigerated system supports controlled processing of temperature-sensitive samples.
Our High-Speed Centrifuge 15,000 RPM is designed for applications requiring efficient and rapid separation at high centrifugal speeds. Across our complete centrifuge range, Labtronixed Inc. emphasizes robust construction, dependable performance, precision, operational convenience, and laboratory safety. Our centrifuges are designed to support a wide variety of applications in biotechnology, microbiology, molecular biology, pharmaceuticals, healthcare, diagnostics, research, and industrial laboratories.
With its extensive range of centrifugation solutions, Labtronixed Inc. provides customers with options according to required speed, temperature control, capacity, sample type, and application. Our commitment is to provide dependable laboratory equipment that combines advanced technology, consistent performance, user-friendly operation, and durable construction to support the requirements of modern laboratories.
Our Product Range
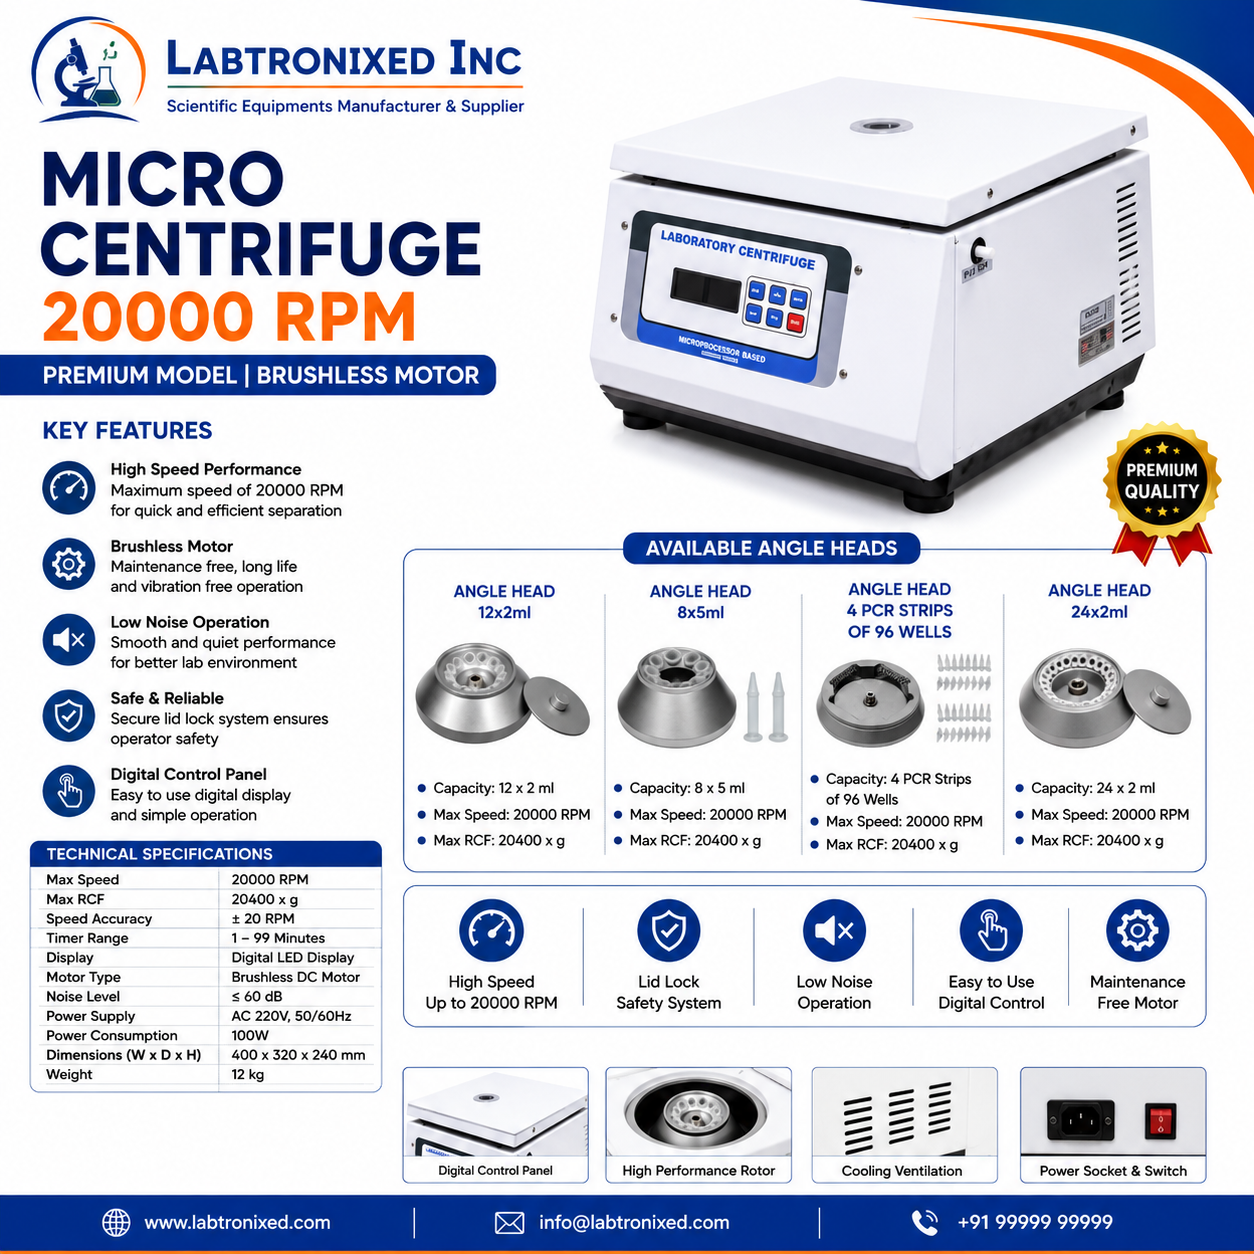
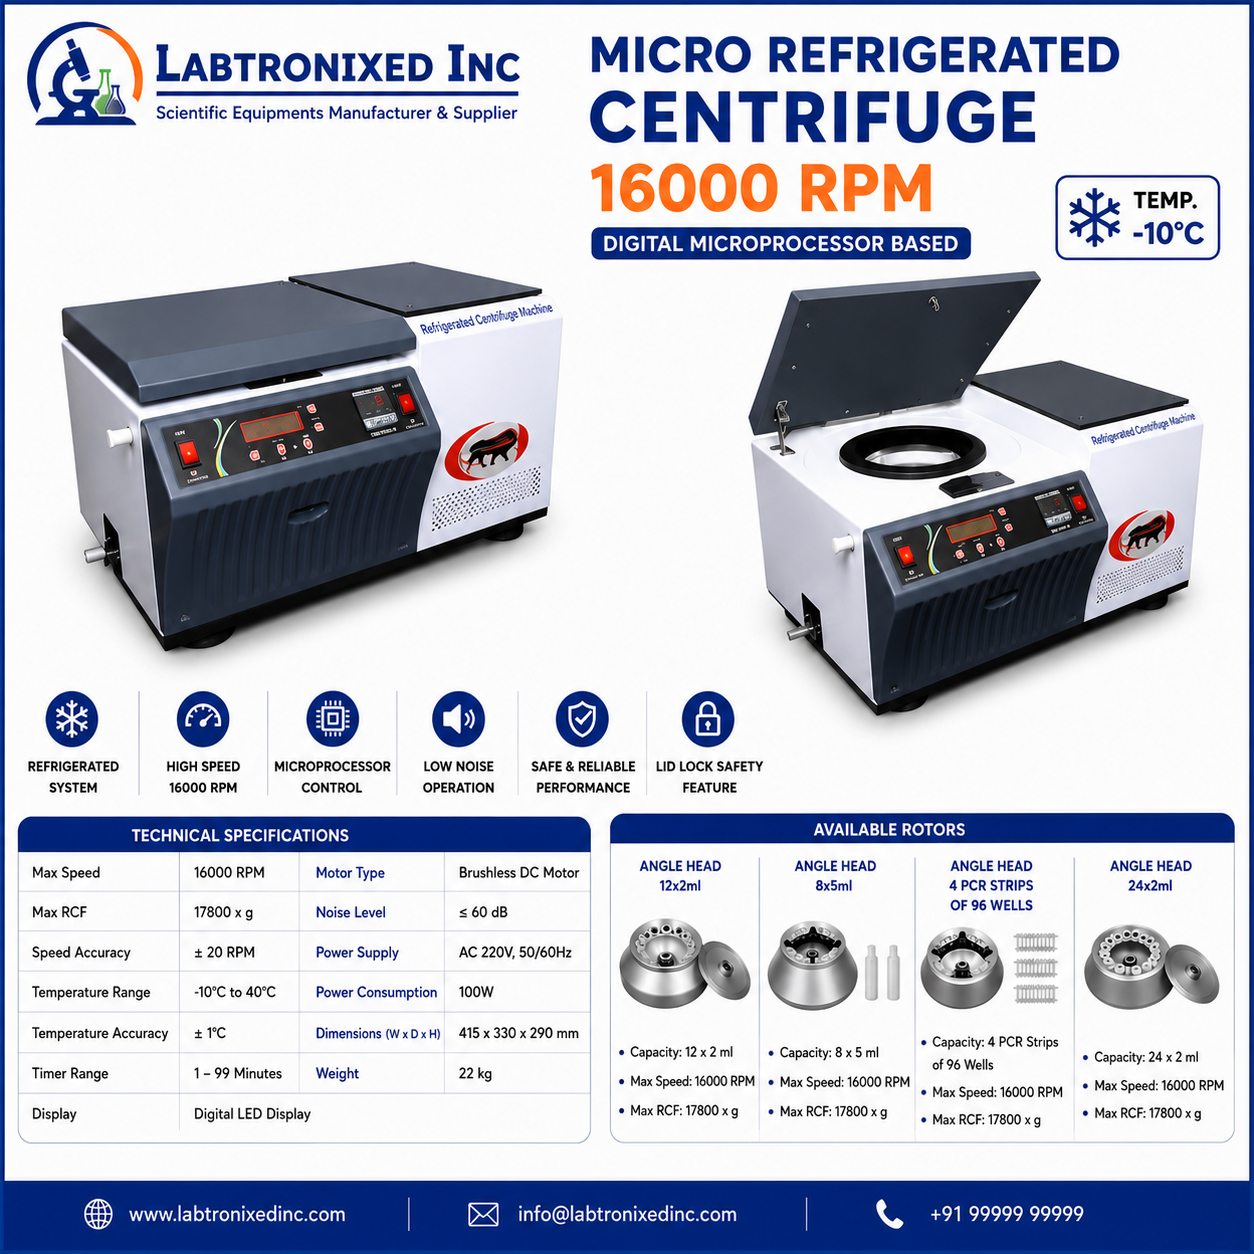
Refrigerated Micro Centrifuge (Digital16000 R.P.M. (Microprocessor Based)
₹0.00

High Speed Refrigerated Micro Centrifuge Digital-20000 R.P.M.(Brushless Motor)
₹0.00
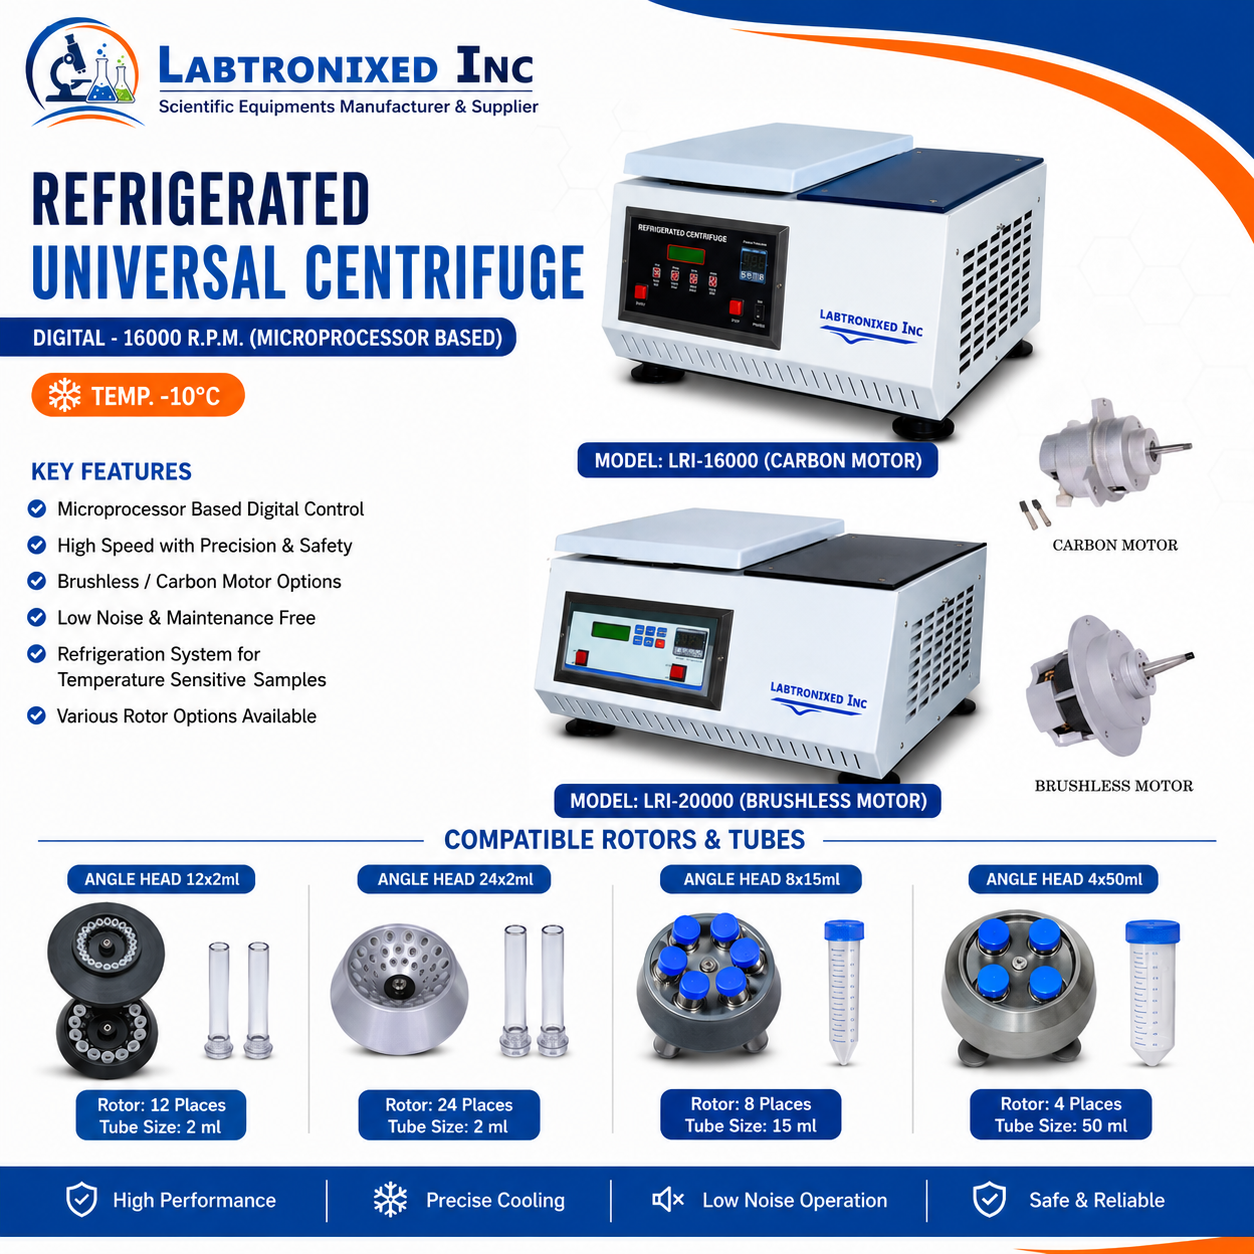
Refrigerated Universal Centrifuge – Digital-16000 R.P.M.(Microprocessor Based)
₹0.00
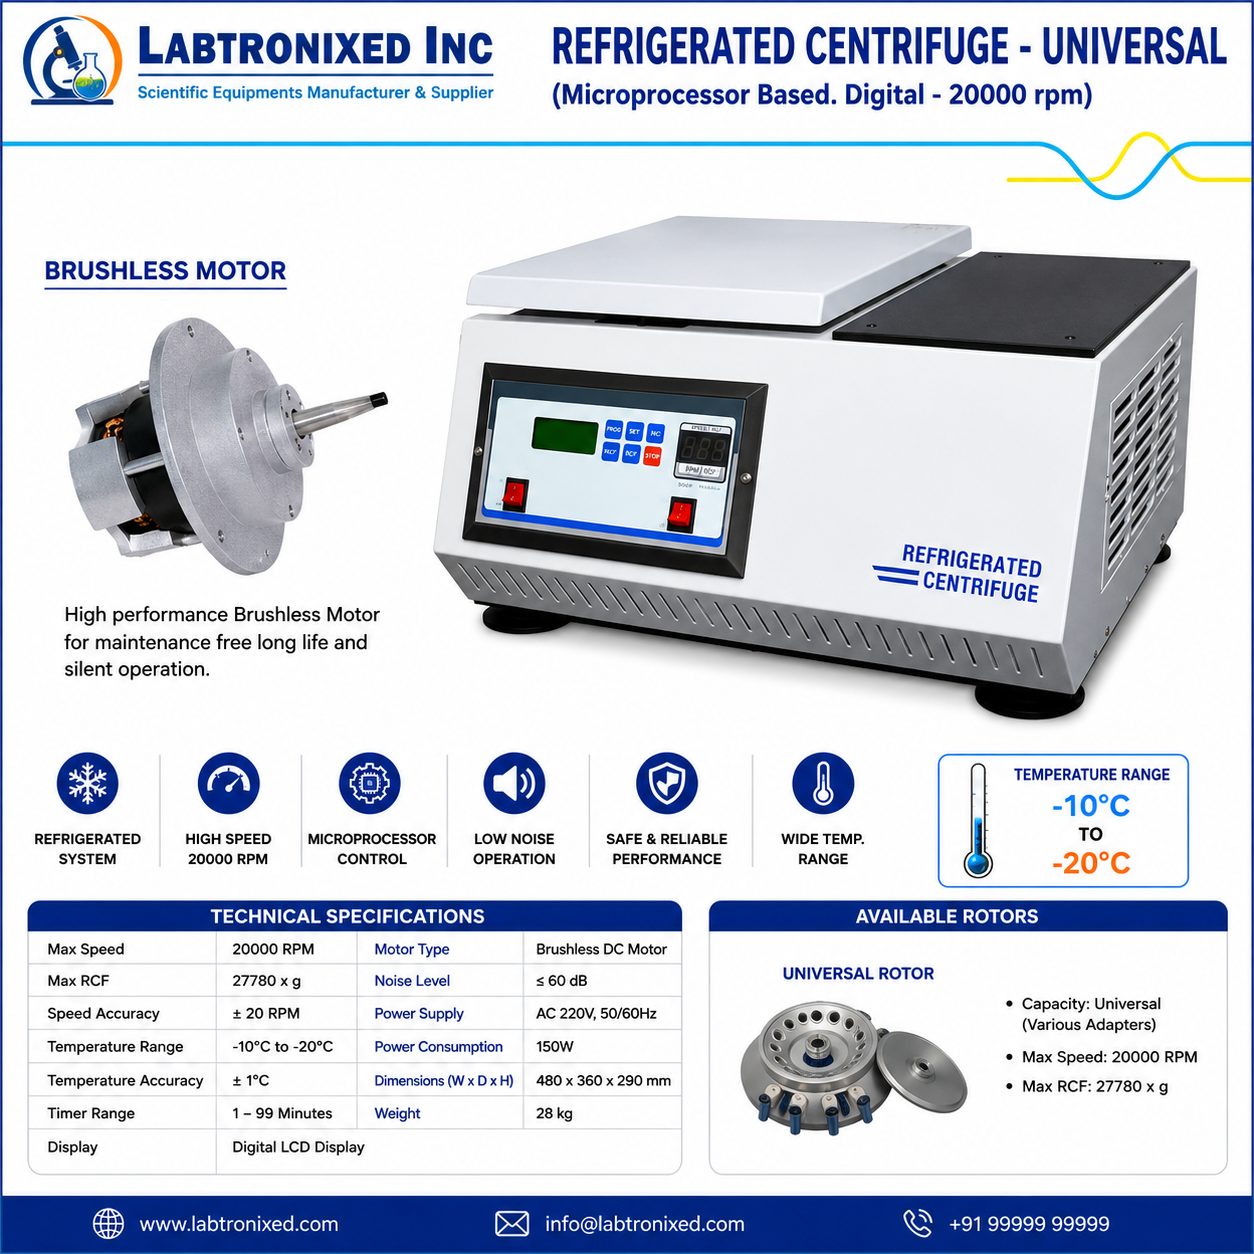
Refrigerated Universal Centrifuge – (Microprocessor Based. Digital - 20000 rpm)
₹0.00
What is an Autoclave?
An autoclave is a high-pressure steam sterilization device used to disinfect medical instruments, laboratory equipment, glassware, culture media, and industrial materials. It works by using saturated steam under controlled pressure and temperature to destroy microorganisms such as bacteria, viruses, fungi, and spores.
Working Principle
The autoclave sterilization process includes:
- Air Removal Phase – Removes trapped air for better steam penetration
- Steam Exposure Phase – High-pressure steam enters the chamber
- Sterilization Phase – Maintains required temperature (121°C–134°C)
- Exhaust & Drying Phase – Releases pressure and dries materials
This ensures complete and reliable sterilization of all loaded materials.
Why Choose Us
- ISO & CE Certified Manufacturing Standards
- Years of Industry Experience
- Customized Sterilization Solutions
- Strong Technical Expertise
- PAN India Supply & Installation
- Operator Training & Support
- Reliable After-Sales Service
- Competitive Pricing
- Industrial & Pharmaceutical Focused Engineering
Customized Sterilization Solutions
We also offer customized autoclave systems based on chamber size, automation level, pressure rating, and specific application requirements. Our team provides complete support including installation, commissioning, validation assistance, and after-sales service across India.
Conclusion
Our advanced autoclaves and ozone sterilizers are designed to deliver maximum sterilization efficiency, safety, and reliability. With a strong focus on innovation, quality, and customer satisfaction, we provide complete sterilization solutions for modern healthcare and industrial needs.
Industries We Serve
We proudly serve:
- Healthcare & Hospitals
- Pharmaceutical Companies
- Research Laboratories
- Biotechnology Industry
- Food & Beverage Sector
- Agriculture & Farming Units
- Educational Institutions
- Industrial Manufacturing Units